Hey there, let’s cut to the chase—if you’re here because you just got your hands on a PE microduct bundle pipe COD pipe machine (or you’re thinking of picking one up soon) and have no clue how to actually operate it without messing up a run or burning out a part, you’re in the right spot. I’ve been supplying these machines for 7 years now, and let’s be real: I’ve seen new operators (and even some old pros) skip a step, end up with wonky microducts that leak when they get pulled, or blow a fuse because they cranked the wrong knob too hard. This isn’t rocket science, but it’s also not just “plug and play” — stick with me, and I’ll walk you through every do, don’t, and tiny trick that’ll save you a headache (and a lot of wasted plastic). PE Microduct Bundle Pipe COD Pipe Machine
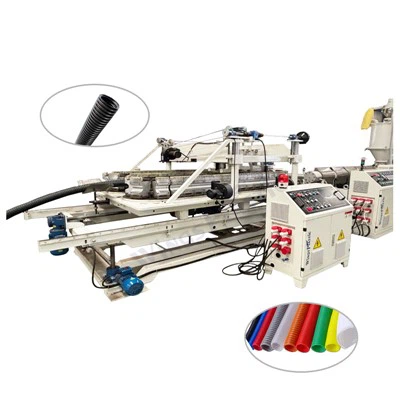
First off, a quick heads up: I’m not gonna bore you with 10-page manuals you’ll never read. We keep these machines simple, because running a factory or job site doesn’t leave time for that. That said, before you even turn the power on, there’s 5 checks that take 2 minutes and will make the rest of the run 10x smoother. Let’s start with materials, because if your PE resin or microduct cores are garbage, even the best operator can’t fix that. I always tell guys to use virgin PE resin (not recycled, unless it’s super clean — I’m talking no crumbs, no dirt, no random bits of other plastic) because recycled can cause clogs in the extruder and mess up the wall thickness of the final pipe. For the bundle cores, make sure they’re the exact size you ordered—if you ordered 7x 4mm ducts, don’t try to stuff 6mm ones in there; that’ll stretch the outer COD pipe too thin and it’ll split when you pull cable through later.
Next, the hopper. This is where you feed the resin, right? But don’t just dump it in—first, give the hopper a quick wipe out to get rid of any leftover dust or old resin from the last run. If there’s even a speck of leftover different plastic, it’ll get pushed through with the new resin and create a weak spot in your pipe. Also, make sure the hopper’s feed screw turns freely when you twist it by hand—if it’s stuck, that means something’s jammed, and turning the power on will just burn out the motor. I’ve seen that happen way too many times.
Then, the cooling system. This is non-negotiable. PE needs to cool slowly and evenly to keep its shape—if you skip this, your pipe will warp like a potato chip and be useless. Before powering on, check both the water lines and the air cooling unit (some machines use water, some use air, most use a mix). For water-cooled units, make sure the inlet pressure is between 0.2 and 0.4 MPa—too high and you’ll crack the pipes, too low and it won’t cool enough. For air, the filter on the compressor shouldn’t be clogged—change it every 500 hours, or if you hear the unit working way harder than normal. Pro tip: run a quick test by holding your hand 6 inches from the cooling die while it’s running—if you feel a blast of warm air or mist, that’s good; if it’s super hot, your cooling’s bad, so fix it before you start.
Now, power up time. Don’t just hit the main switch and go. Start with the control panel: turn all the zone heaters to 160°C first, then wait 10 minutes, then crank them up to the proper temperature. Wait, what’s the proper temp? It depends on the PE grade, but for standard MDPE (the stuff we use for most COD pipes), 185–200°C is sweet. If you go above 210°C, you’ll burn the resin, and it’ll smell like burnt plastic, create black specks in your pipe, and ruin the extruder. Also, let the heaters hold that temp for another 10 minutes after hitting the mark—this ensures all the resin passages are hot evenly, so you don’t get cold spots that cause lumpy walls.
Last pre-run check: the haul-off unit. That’s the part that pulls the pipe through the machine, right? The tension rollers should be set for the diameter of your pipe. If they’re too loose, the pipe will bow or wrinkle; too tight, and you’ll stretch the outer wall so thin it breaks. I use a quick test here: when the heaters are holding temp, crank the haul-off to low speed (like 5 meters per minute, not the max 50) and pull a 1-meter test length. Hold it up to light—if you see any gaps in the wall or it’s lumpy, you need to adjust the die gap (more on that in a sec). If it’s smooth, you’re good to start.
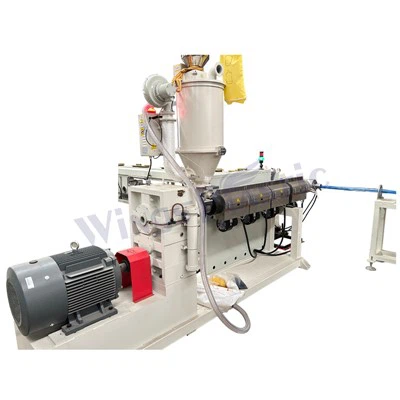
Okay, pre-run checks done—now let’s get to the actual run, and this is where most people mess up. First, the extrusion zone: when you feed resin into the hopper, start the extruder at 20 RPM. Don’t go higher until you see steady, uniform plastic coming out of the die head. If it’s coming out in blobs or has air bubbles, that means you have a clog, the heaters aren’t hot enough, or there’s air trapped in the resin. Stop immediately and clear it—don’t just keep cranking, because that’ll push the clog through and break the die.
Once you’ve got a steady stream of plastic coming out, feed your microduct cores into the center of the die. Here’s the thing: you need to make sure they’re aligned perfectly, not touching the inner walls of the outer pipe. If they rub, they’ll scuff, and that will make it impossible to pull cable through later (we call that “duct drag” and it’s a nightmare for telecom guys). I use a small laser pointer mounted next to the die to line up the cores—cheap, works like a charm. If you don’t have a laser, just eyeball it: the cores should be evenly spaced around the center, no leaning to one side.
Now for the haul-off speed. This is a balance, not a set number. The goal is to match how fast the extruder is pushing plastic to how fast the haul-off is pulling. If you extrude 10kg of plastic per minute and the haul-off is going too fast, the pipe will get stretched so thin it’s weak. Too slow, and the plastic will pile up at the die, making a big bulge that breaks off or warps. How do you adjust this? Keep an eye on the pipe’s diameter gauge (most machines have an inline one now). The diameter should be dead on what you ordered—say, 32mm outer diameter. If it’s under, speed up the haul-off a tiny bit. If it’s over, slow it down. Simple, right? Wait, no—there’s also the cooling. If you run the haul-off too fast, the cooling might not keep up, so you might need to turn the cooling water pressure up a notch to keep the shape. It’s a back-and-forth, that’s why the test run at low speed is so important.
Another thing to watch for during a run: the pressure gauge on the extruder. It should sit between 12 and 18 MPa for standard COD pipes. If it spikes above 20 MPa, that means there’s a clog somewhere—either in the hopper feed, the extruder screw, or the die head. Stop the run, let the pressure drop, then take apart the die and clear the clog. I can’t tell you how many guys ignore that pressure spike and blow a $2,000 die head because they kept running. Don’t be that guy.
Now, what about common mistakes I see all the time? Let’s run through the big ones so you can avoid them. First, don’t leave the machine running unattended. I know, job sites are busy, but 10 minutes is all it takes for the cooling to fail, or a core to slip, or a pressure spike to blow something up. If you have to step away, set the machine to idle (low speed, heaters at 150°C) instead of shutting it off, but never leave it alone for more than 5 minutes. Second, don’t use too much lubricant. Some guys think “more lube = smoother run,” but no—too much lube gets into the pipe, messes up the plastic’s strength, and makes it so when you pull cable through, the lube attracts dirt and causes leaks. We use a food-grade PE-compatible lube, and only a thin coat on the die head—never on the cores. Third, don’t forget to clean the machine after every run. Even if you’re doing the same product next, a quick wipe of the die, hopper, and haul-off rollers will keep it running for years. If you leave old resin in the extruder, it’ll harden and cause clogs next time.
Wait, what about start-up and shut-down procedures? People skip this all the time, and that’s why they have machine breakdowns. Start-up, we already covered, but shut-down is just as important. When you’re done with a run, first stop feeding cores into the die, then let the extruder keep running for 2 more minutes to push all the resin out of the die. Then, turn the heaters down to 150°C, keep the cooling running for 10 more minutes, then turn the main power off. If you just shut everything off hot, the resin will harden in the die, and next time you start up, you’ll have to take the die apart and drill out the hardened plastic. That’s a 2-hour job, trust me.
Oh, and a quick note on troubleshooting common issues, because you’re gonna run into something at some point. If your pipe has air bubbles: your resin has moisture in it. Dry the resin in a hopper dryer at 80°C for 4 hours before using it. If your pipe has lumpy walls: your heaters are uneven, or the die gap is off. Adjust the die screws a quarter turn at a time, no more. If the cores are shifting during the run: the core feed tension is off. Tighten the core feed rollers just a tiny bit so they don’t slip.
Now, a quick reality check. I sell these machines to small telecom installers and big construction firms alike, and the guys who follow these steps run for 10 years with minimal issues. The ones who skip the pre-run checks, crank the speed too high, and leave the machine running unattended? They’re calling me every month for a replacement part or a service call. This isn’t rocket science—it’s just following simple steps, and paying attention.
If you’re looking to pick up a machine, or you have one already and need help with a specific run, hit me up. I don’t do fancy sales pitches—just straight talk, because I’ve been in this industry long enough to know that a happy customer is one who’s making good pipe, not one who’s dealing with headaches. Don’t overcomplicate this: take 2 minutes to check the basics, run a low-speed test, adjust as you go, and clean up after yourself. That’s it. If you have questions, or you’re ready to find a machine that fits your production needs, just reach out—no pressure, no hidden fees, just honest advice.
PPR Pipe Machine References:
- Modern Extrusion Technology, Society of Plastics Engineers, 2019
- PE Microduct and COD Pipe Manufacturing Guidelines, International Telecommunications Energy Conference, 2021
- Industrial Plastic Extrusion Machine Operation and Maintenance Handbook, Elsevier, 2020
Qingdao Wings Plastic Technology Co., Ltd.
As one of the most experienced pe microduct bundle pipe cod pipe machine manufacturers and suppliers in China, we also support customized service. Please feel free to buy durable pe microduct bundle pipe cod pipe machine made in China here from our factory. For price consultation, contact us.
Address: C02 Of Anshengyi Road, No.2 Fuan Industry Zone,Jiaodong Town, Jiaozhou City, Qingdao City, Shandong Province,China
E-mail: kelly@wingsplastic.com
WebSite: https://www.wingsextruder.com/
