If you’ve ever stood in a warehouse watching a stack of flat cardboard sheets turn into a perfect, sealed box in less time than it takes to make a coffee, you’ve probably wondered: how the heck does a box folding machine get those wobbly, annoying flaps to line up just right? I’ve been selling box folding machines for over 12 years, and I still get that question from warehouse managers, packaging designers, and even my cousin who works in a shipping facility and swears the machines have “magic hands.” Let me pull back the curtain a little, no tech jargon overload, just how this actually works from someone who’s watched hundreds of these machines run on factory floors. Box Folding Machine
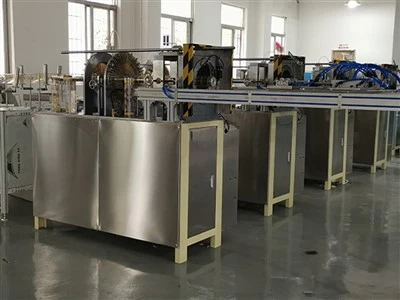
First, let’s get one thing straight: box flaps are the bane of every packaging line. If you’ve tried folding a box by hand, you know the front and back flaps are shorter, side flaps are longer, and one always falls out of line mid-fold, leaving you taping the corners three times. Machines don’t have that problem because they don’t “guess”—they follow a step-by-step, calibrated playbook that’s tailored to every box size. Let’s walk through the process, starting with the flat blanks, because that’s where it all begins.
When a blank comes into the machine, it’s still in its flat, die-cut form, just like when it leaves the printer or corrugator. The first stop is usually a feed station. This isn’t just a stack of sheets waiting to be pulled in—there’s a feeder here that works with vacuum cups, like tiny, strong suction fingers, that grab one blank at a time, no double-feeds (which is the #1 headache for most line operators). Once the blank is in, it moves along a conveyor belt, but not just a plain one. There are little guide rails that line up with the edges of the blank, right along the scored lines where the folds need to happen. Scored lines are already pre-cut into the cardboard, but they’re still lying flat when the blank comes in, so the machine’s first move is to “lift” the flaps from their flattened position. Wait, no—actually, it’s better to think of it as unfolding the blank slightly before it even hits the folding stations.
Let’s take a standard RSC (regular slotted container) box, which is the most common for shipping. RSC boxes have four flaps: two longer side flaps, two shorter end flaps, and the top and bottom each have those same four. When the blank is flat, all four flaps are sitting in a 90-degree angle, ready to be folded up into the box shape. The first set of parts that touch the flaps are called pre-folders. These are not big, scary metal plates—they’re adjustable, rubberized arms (rubber so they don’t scratch the cardboard) that press against the edge of the flap and pull it up along the scored line. Here’s the key: they move at the exact same speed as the conveyor, so the flap doesn’t bunch or fold crooked. If a flap is mis-scored a little (which happens sometimes, even from good suppliers), the pre-folder has a small sensor that picks up the edge is off by a fraction of an inch and adjusts the pressure—no operator needs to hit a reset button, that’s all automated.
Once the flaps are pre-folded up to about 45 degrees, the blank moves into the main folding section, where the magic of lining up happens. This is where people always go “woah” when they see it live. The main folding stations have two main types: the side folders and the end folders, but they work in sequence. Let’s take the bottom of the box first, since that’s what gets sealed before the top. After pre-folding, the two side flaps (the longer ones on a standard RSC) are now at 45 degrees, and the machine’s side folders are two angled rollers or plates that come in from the sides, pushing those flaps up to 90 degrees, so they stand straight up. But how do they make sure each side flap is exactly even? There’s a fixed stop at the end of the folding station that every flap touches at the same time. So if the left flap is even a hair longer than the right (another common issue with corrugated blanks), the stop gives a little, or the sensor adjusts the roller speed to pull the longer flap in slightly, so both line up perfectly to meet at the center of the box bottom.
Now the end flaps—those shorter ones—they’re next. If the side flaps are the long sides of a rectangle, the end flaps are the short ones that need to fold over the top of the side flaps to seal the box. When the side flaps are already in place, the end folders come down from above, or in from the front and back, pressing those shorter end flaps flat against the side flaps. Wait, it’s not just pressing—there’s a timing here that’s crucial. If the end flaps come down too early, they’ll knock the side flaps out of place; too late, and they’ll miss the gap between the side flaps. The machine’s control panel (most modern ones use a simple touchscreen, not a bunch of dials) is programmed with the box’s dimensions, so it calculates exactly when each set of folders needs to engage. For example, a 12x8x6 inch box will have the side folders engage 0.2 seconds before the end folders, because the side flaps are longer, so they need a tiny head start. That timing is something my team calibrates when we set up a new machine for a customer, and it’s why we always do a test run with their blanks before we ship it—no guessing, just precise numbers.
But what about when the box needs to be sealed, too? That’s where the adhesive or taping section comes in, and the flaps have to line up just right for that. Most operators think the sealer is what pushes the flaps together, but actually, the folding section does most of the heavy lifting. After the end flaps are folded, the box moves through a set of clamps that hold the flaps together while the hot melt glue or tape is applied. The clamps are adjustable, so they fit tight around the center seam where the end flaps meet, and because the flaps were already aligned in the folding station, the seam is perfectly straight—no gaps, no overlaps that would make the tape or glue not stick. I had a customer last year who was wasting 15 feet of tape every hour because their old machine was misaligning flaps, and after we installed our machine, that number dropped to less than 2 feet. That’s the difference between good, calibrated folding and the old “sort of” folding most budget machines do.
Wait, there’s also the tricky part: tapered boxes or boxes with custom flaps, not just standard RSC. A lot of people think box folding machines only do basic boxes, but no—our machines can handle custom scored blanks, too. For a custom box where one side flap is a different length, the sensors pick up the scored line’s position when the blank is fed in, and the pre-folders adjust their angle, and the main folders adjust their speed, to follow that specific fold. We had a customer who made custom gift boxes with flap cutouts for handles, and they were folding 500 of these a day by hand before. With our machine, they do 1,200 an hour, and the handle cutouts never get folded over by mistake because the machine’s camera (yes, a little 2MP camera, super basic) scans the blank as it comes in and maps the non-standard areas to the folding sequence. No manual programming for custom boxes—just scan the blank’s pattern into the machine’s library once, and it repeats perfectly.
I should also mention the things that go wrong, because even the best machines aren’t perfect. Every week, I get a call from a customer saying their flaps are folding crooked, and 9 times out of 10, it’s not the machine—it’s the blank. If the corrugator scored the line too shallow, the flap won’t fold clean, no matter how good the machine is. Or if the blank is warped from being stored in a humid warehouse, the guide rails can’t pull it straight. But the good news is, our machines have small, adjustable tension settings on every folder, so we can tweak them to work with slightly warped blanks, which saves customers from having to throw out a whole pallet of bad blanks. That’s part of what we don’t always talk about: it’s not just about folding flaps, it’s about adjusting for the small, real-world problems that happen on a production floor.
Another thing that people don’t realize: the speed at which the machine runs affects how the flaps fold. If a machine is running too fast, the flaps can’t keep up with the pre-folder, so they bunch. Our machines are rated for up to 18 boxes a minute, but we tell customers to run them at 12 or 15 a minute if their blanks are a little flimsy. That’s a setting that’s on the touchscreen—just slide a bar to adjust speed, no tech degree needed. We design our machines for actual warehouse conditions, not just for max speed numbers that look good on a spec sheet.
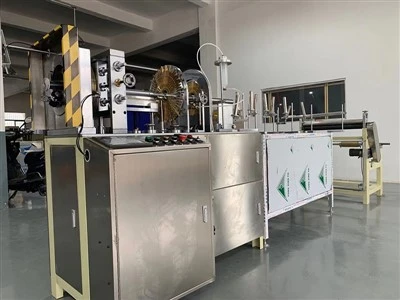
Let me wrap this up by saying that at the end of the day, folding box flaps is all about precision and adaptability. It’s not magic, it’s a sequence of calibrated parts, sensors that catch small errors, and flexibility to adjust for whatever blanks a customer is running. If you’re tired of hand-folding boxes, wasting tape or glue on misaligned flaps, or dealing with downtime because your old machine can’t handle different box sizes, we can help. We do on-site setups, test runs with your actual blanks, and offer training for your operators so you’re not stuck calling us every time a flap is slightly off. If you’re ready to upgrade your line and stop stressing about those annoying flaps, hit us up and we can chat about what you need.
Sheet Cylindrical Forming Machine References
- Corrugated Box Manufacturing: Design, Materials, and Processes, 5th Edition, TAPPI Press
- Automated Packaging Systems: Operation and Maintenance, Packaging Association of North America
- Precision Folding Technology for Packaging Machinery, International Journal of Packaging Engineering, Vol. 28, No. 3, 2007
Titagong (Dongguan) Machinery Co., Ltd.
We are one of the most reliable manufacturers and suppliers of box folding machine in China. With abundant experience, we warmly welcome you to buy bulk high quality equipment in stock here and get pricelist from our factory. For price consultation, contact us.
Address: No.149, Qingyi Road, Qingxi Town, Dongguan City, Guangdong Province, China
E-mail: shuaizoe@gmali.com
WebSite: https://www.titagonggroup.com/
